Quality Control in Paper Carrier Tape Packaging: 12 Key Inspection Checks
Electronic components can pass electrical testing and dimensional inspection but still cause production problems if they are packaged incorrectly. Empty pockets, reversed components, unstable sealing, paper dust, excessive component movement, and poor reel winding can interrupt SMT assembly and increase rejection rates.
For this reason, quality control in paper carrier tape packaging should not be limited to a final visual inspection. It should cover the complete process, including incoming material inspection, pocket forming, component loading, cover tape sealing, reel winding, labeling, and final feeder validation.
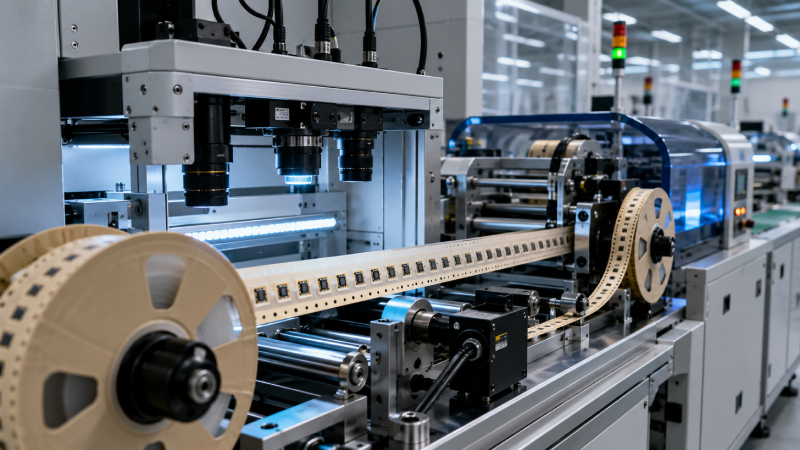
A reliable quality-control system helps component manufacturers reduce packaging defects, protect delicate components, and deliver reels that run smoothly on automated placement equipment.
What Does Paper Carrier Tape Quality Control Include?
Paper carrier tape quality control is a structured inspection process used to confirm that the tape, pockets, components, cover tape, and reels meet the approved packaging requirements.
The main inspection stages normally include:
-
Base paper thickness and material consistency
-
Pocket dimensions and punching quality
-
Sprocket-hole position and pitch
-
Tape flatness and dimensional stability
-
Component presence and orientation
-
Component movement inside the pocket
-
Cover tape alignment and sealing quality
-
Peel force consistency
-
Reel winding direction and tension
-
Quantity, labeling, and traceability
-
Final feeder compatibility
Each stage controls a different risk. A tape may look acceptable but still fail during high-speed feeding because of accumulated pitch error, excessive peel force, or poor component positioning.
Why Paper Carrier Tape Needs a Dedicated Quality-Control Plan
Paper carrier tape is widely used for small electronic components such as resistors, capacitors, inductors, and other passive devices. It offers good processing efficiency and is often suitable for high-volume tape-and-reel packaging.
However, paper behaves differently from embossed plastic materials. Its performance can be influenced by fiber structure, moisture, punching conditions, storage environment, and mechanical stress.
Typical paper-specific risks include loose fibers, punching burrs, torn pocket edges, thickness variation, moisture absorption, delamination, tape deformation, and tearing during feeding.
The quality-control plan should therefore be developed according to the actual component and packaging requirements. Important factors include component dimensions, weight, sensitivity, tape width, pocket design, cover tape type, packaging speed, storage conditions, and the customer’s acceptance criteria.
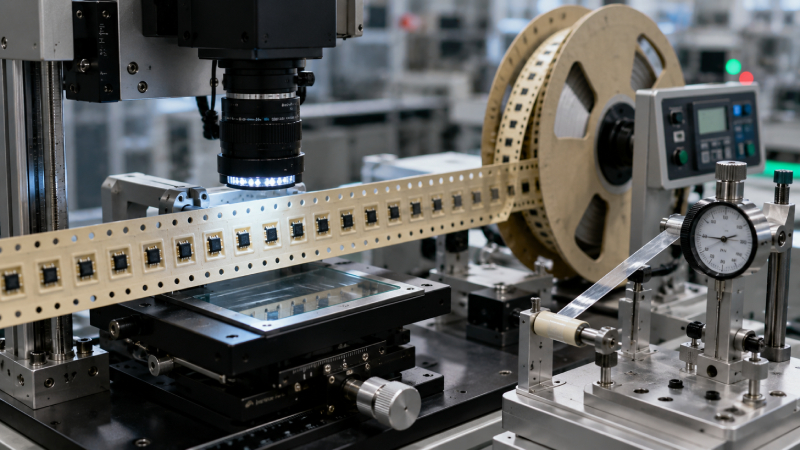
12 Critical Quality Checks in Paper Carrier Tape Packaging
1. Base Paper Thickness and Material Consistency
The quality process begins before any pockets are punched.
Incoming paper tape should be checked for total thickness, thickness variation, surface consistency, flatness, layer bonding, and visible contamination. Creases, dents, uneven edges, or weak areas may affect the later punching and sealing processes.
Inconsistent material thickness can change pocket depth, sealing pressure, and feeder movement. Manufacturers should inspect different positions across the roll rather than measuring only one point.
2. Moisture and Dimensional Stability
Paper-based materials can absorb moisture from the surrounding environment. Changes in moisture may influence tape dimensions, stiffness, flatness, and punching performance.
Materials should be stored under controlled conditions and allowed to stabilize before precision measurement or packaging. Quality teams may compare tape dimensions before and after environmental conditioning when the application has strict stability requirements.
The acceptable moisture condition should be based on the approved material specification rather than a single universal limit.
3. Pocket Dimensions
Pocket dimensions determine whether the component sits securely and can be picked up reliably.
The most important dimensions commonly include A0, B0, and K0. A0 and B0 define the pocket opening, while K0 relates to the effective pocket depth.
If the pocket is too small, the component may become stuck, scratched, or difficult to load. If it is too large, the component may rotate, tilt, or move excessively during transport and feeding.
Pocket dimensions should be checked against the approved tape drawing and component tolerances.
4. Pocket Pitch and Sprocket-Hole Accuracy
SMT feeders depend on the sprocket holes to index the tape accurately. Quality inspection should cover pocket pitch, sprocket-hole pitch, hole diameter, edge distance, and the position of each pocket relative to the holes.
A small error in one position may appear harmless. However, repeated errors can accumulate along the tape and cause unstable indexing or pickup-position variation.
Optical measuring equipment is often used when the required tolerances cannot be reliably verified with basic manual tools.
5. Pocket Edge Quality and Burr Control
Punching paper tape may create raised fibers, loose particles, torn edges, incomplete cavities, or delamination around the pocket.
These defects can prevent the component from sitting correctly. Loose fibers may also contaminate the component or enter sensitive production equipment.
Punching tools should be inspected and maintained regularly. Worn tooling, incorrect clearance, unsuitable material, or poor cleaning can increase burr formation. Pocket edges and sprocket holes should be sampled throughout production, not only during the first setup.
6. Tape Flatness and Camber
A carrier tape should remain flat and track smoothly through feeding equipment.
Inspectors should check for sideways curvature, twisting, edge waviness, local bending, and deformation around the punched pockets. Excessive camber can cause the tape to move away from the intended feeder path.
Flatness problems may result from material variation, incorrect winding tension, storage conditions, or unstable punching pressure.
7. Component Presence and Quantity
Every required pocket should contain the correct component unless empty pockets are specifically allowed by the customer’s packaging specification.
The inspection system should identify empty pockets, double-loaded pockets, broken components, incorrect parts, and quantity differences.
Automated counters and machine-vision systems can provide continuous monitoring, while manual checks at the beginning and end of the reel provide additional confirmation. Production records should match the final labeled quantity.
8. Component Orientation and Polarity
Incorrect orientation is one of the most serious tape-and-reel packaging defects.
The inspection system should verify loading direction, polarity, pin-one position, top and bottom orientation, and rotation angle. An approved orientation drawing or golden sample should be available at the packaging station.
For polarized or asymmetric components, orientation should be checked automatically where possible. A correctly sized pocket cannot prevent errors if the component is loaded in the wrong direction.
9. Component Movement Inside the Pocket
A component may be present and correctly oriented but still move too much inside the cavity.
Quality checks should evaluate lateral movement, vertical movement, rotation, tilting, contact with pocket walls, and the possibility of the part sticking to the cover tape.
Excessive movement can change the pickup position or damage the component during transportation. Movement limits should be confirmed during sample approval and actual feeder trials.
10. Cover Tape Alignment and Seal Continuity
The cover tape should be centered and sealed continuously along the carrier tape.
Inspectors should check seal-track position, seal width, wrinkles, gaps, contamination, premature lifting, and damage above the component pockets. The cover tape should protect the components without interfering with their position.
Incorrect guide settings, unstable tension, uneven heat, or contamination in the sealing area can create weak sections along the reel.
11. Peel Force and Peel Consistency
Peel force is the amount of force required to remove the cover tape from the carrier tape.
If the force is too low, the cover tape may lift during winding, transportation, or handling. If it is too high, peeling may create vibration, sudden movement, tape tearing, or feeder interruption.
Testing should consider peel angle, test speed, tape width, cover tape type, sealing temperature, pressure, and dwell time. Engineers should evaluate variation along the reel instead of relying only on one average value.
The required peel-force range should be defined for the specific tape and cover tape combination.
12. Reel Winding, Leader, Trailer, and Labeling
Final inspection should confirm that the completed tape is wound in the correct direction with controlled tension and aligned edges.
Quality teams should look for telescoping, loose winding, crushed pockets, bent flanges, damaged reels, and tape shifting. Leader and trailer lengths should meet the agreed packaging requirements.
Labels should clearly identify the part number, lot number, component quantity, orientation, production date, and inspection status. This information supports traceability if a problem is discovered later.
Inspection Methods and Equipment
Manufacturers may use several inspection methods throughout the packaging process.
Dimensional inspection can involve thickness gauges, measuring microscopes, optical comparators, digital gauges, and dedicated carrier tape measurement systems. The selected method should be accurate enough for the drawing tolerances.
Automated machine vision is commonly used to detect missing components, incorrect orientation, excessive rotation, visible damage, pocket contamination, and cover tape misalignment.
Peel testers measure cover tape removal force under controlled conditions. The quality team should review average values, maximum and minimum results, sudden force spikes, and variation between different reel sections.
Mechanical and environmental testing may include tensile testing, tear testing, humidity conditioning, storage simulation, reel rotation, or transportation testing.
A final feeder trial is especially valuable for new components or new pocket designs. It can reveal indexing, peeling, pickup, and tape-tracking problems that may not be visible during static inspection.
Common Packaging Defects and Corrective Actions
| Defect | Possible Cause | Corrective Action |
|---|---|---|
| Empty pockets | Interrupted component feeding | Adjust loading equipment and vision detection |
| Component rotation | Excessive pocket clearance | Optimize pocket dimensions |
| Paper burrs | Worn punching tools | Maintain tooling and improve cleaning |
| Weak sealing | Low sealing temperature or pressure | Revalidate sealing parameters |
| Excessive peel force | Too much heat or pressure | Reduce sealing energy or review cover tape |
| Wrinkled cover tape | Misalignment or unstable tension | Correct guide and tension settings |
| Tape camber | Material or storage variation | Improve material and storage controls |
| Loose winding | Incorrect reel tension | Standardize winding parameters |
Corrective action should address the root cause rather than simply removing defective reels. Repeated defects should trigger process review, tool inspection, parameter adjustment, and verification of the improved result.
Building a Reliable Quality-Control Plan
An effective control plan normally includes three stages.
Incoming quality control verifies paper tape, cover tape, reels, labels, and material documentation. In-process quality control covers first-article inspection, dimensional sampling, component vision inspection, sealing parameter monitoring, and peel testing.
Outgoing quality control confirms reel appearance, winding direction, quantity, label accuracy, packaging integrity, and traceability records.
Inspection frequency should be based on production risk, process capability, component sensitivity, and customer requirements. New tools, new materials, new component designs, and adjusted sealing settings may require additional inspection.
How to Evaluate a Paper Carrier Tape Packaging Supplier
A capable supplier should be able to explain how quality is controlled, not simply claim that the product is inspected.
Buyers should ask whether the supplier can design pockets from component drawings or samples, provide dimensional inspection reports, control paper dust and burrs, inspect component orientation automatically, record sealing parameters, test peel force, and perform feeder trials.
It is also important to confirm whether production lots are traceable and whether pilot reels can be supplied before mass production.
For a new component, the supplier should evaluate pocket dimensions, movement allowance, loading orientation, cover tape compatibility, reel requirements, and the final inspection standard before full production begins.
Frequently Asked Questions
What is inspected during paper carrier tape packaging?
The inspection normally covers carrier tape material, pocket dimensions, sprocket holes, burrs, component presence, orientation, movement, cover tape sealing, peel force, reel winding, quantity, and labeling.
Which paper carrier tape dimensions are most important?
Important dimensions include pocket width, length, depth, pocket pitch, sprocket-hole pitch, hole position, edge distance, and total tape thickness.
Why do paper burrs appear around the pockets?
Common causes include worn punching tools, incorrect tooling clearance, material variation, unstable punching conditions, and insufficient cleaning.
Can machine vision detect every packaging defect?
Machine vision is effective for visible defects such as missing parts and incorrect orientation. However, dimensional measurement, peel testing, mechanical inspection, and feeder validation are still required.
Is compliance with a general packaging standard enough?
No. Industry standards provide a useful foundation, but each component may require its own pocket dimensions, orientation rules, movement limits, sealing parameters, and acceptance criteria.
What documents should buyers request?
Useful documents include the approved tape drawing, orientation drawing, first-article inspection report, peel-force report, final inspection record, and lot traceability information.
Conclusion
Quality control in paper carrier tape packaging should begin with material selection and continue through punching, loading, sealing, winding, and final release.
Reliable packaging depends on accurate pockets, clean edges, correct component orientation, controlled movement, stable peel force, and complete traceability. These controls help prevent feeder interruptions, component damage, and assembly defects.
When developing packaging for a new resistor, capacitor, inductor, or other small electronic component, manufacturers should validate the complete tape-and-reel system before mass production. A well-designed inspection plan provides greater reliability for both the component supplier and the final SMT assembly line.
The article is structured for approximately 1,300–1,500 words and can be used directly for the next SEO, image, or Markdown publishing step.

 Emial
 John Mr